
A guide to the Lincoln Electric Pulse-on-Pulse GMAW process for welding thin aluminum, detailing features, equipment, and applications.
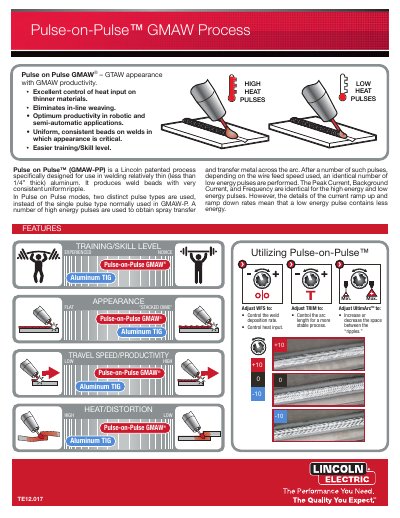
This document describes the Pulse-on-Pulse™ (GMAW-PP) process, a Lincoln Electric patented method designed for welding relatively thin aluminum (less than 1/4" thick). The process utilizes two distinct pulse types—high energy and low energy—to produce weld beads with very consistent uniform ripple, offering excellent control of heat input and eliminating the need for in-line weaving.
| Material Thickness | less than 1/4" thick |
|---|---|
| Wire Diameter | 3/64 in (1.2 mm) |
| Compatible Power Sources | Power Wave i400, Power Feed SA, POWER MIG 350 MP, Power Wave C300, S350, i400 & S500, INVERTEC V350-PRO |
It is specifically designed for use in welding relatively thin aluminum.
It uses two distinct pulse types (high and low energy) instead of the single pulse type normally used in GMAW-P.