PRET PP/PE‑TD20 C3322T‑FNS is a high‑flow, impact‑resistant, anti‑stick polypropylene material for automotive interior parts, with detailed technical…
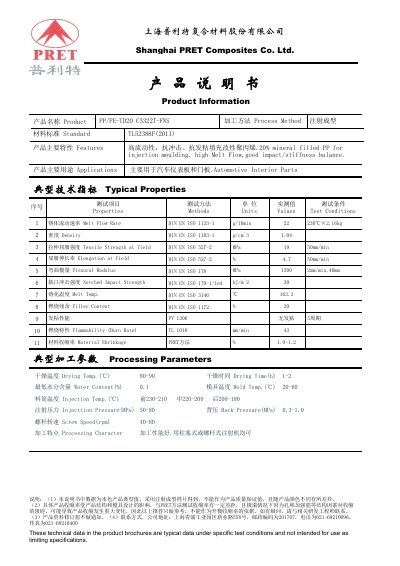
The PRET PP/PE‑TD20 C3322T‑FNS material is a 20% mineral‑filled polypropylene designed for injection molding. It offers high melt flow, good impact resistance, stiffness balance, and no stickiness, making it suitable for automotive interior components such as instrument panels and door panels.
The datasheet provides typical technical specifications (melt flow rate, density, tensile strength, etc.) and recommended processing parameters (drying temperature, injection temperature, mold temperature, pressure, screw speed). Values are typical under the stated test conditions and should be used as reference for product development and molding setup. This manual is written in Chinese.
| Melt Flow Rate | 22 g/10 min |
|---|---|
| Density | 1.04 g/cm³ |
| Tensile Strength at Yield | 19 MPa |
| Elongation at Yield | 4.7 % |
| Flexural Modulus | 1500 MPa |
| Notched Impact Strength | 30 kJ/m² |
| Melt Temperature | 163.3 °C |
| Filler Content | 20 % |
| Material Shrinkage | 1.0‑1.2 % |
| Flammability (Burn Rate) | 43 mm/min |
| Drying Temperature | 80‑90 °C |
| Injection Temperature | 230‑180 °C |
| Mold Temperature | 20‑60 °C |
| Injection Pressure | 50‑80 MPa |
| Screw Speed | 40‑80 rpm |
It is primarily used for automotive interior parts such as instrument panels and door panels.
The melt flow rate is 22 g/10 min.
Injection molding is the recommended processing method, compatible with both plunger‑type and screw‑type injection machines.
Dry the material at 80 °C to 90 °C for 1–2 hours.