
The FabCO XTREME B2 AWS E81T5-B2M H8 datasheet details the gas‑shielded flux‑cored welding wire’s composition, mechanical properties and recommended welding…
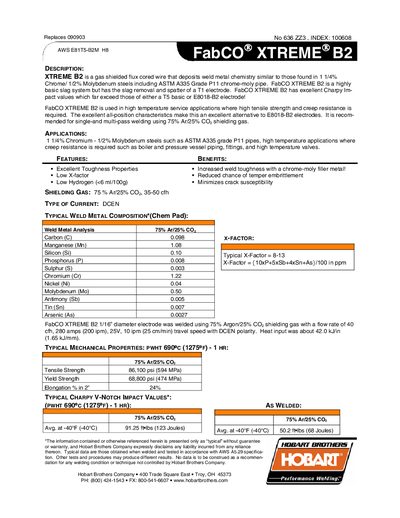
FabCO XTREME B2 is a gas‑shielded flux‑cored welding wire designed for high‑temperature service applications, especially 1¼% Cr‑½% Mo steels such as ASTM A335 Grade P11 pipe. It offers excellent Charpy impact values, low hydrogen content, and good all‑position weldability, making it suitable for boiler, pressure‑vessel piping, fittings and high‑temperature valves.
The datasheet provides typical chemical composition, mechanical properties, and welding parameters. Recommended shielding gas is 75% Ar/25% CO₂ with DCEN polarity, and a range of current, voltage and wire‑feed settings are listed for various positions and diameters.
| Tensile Strength | 86,100 psi (594 MPa) |
|---|---|
| Yield Strength | 68,800 psi (474 MPa) |
| Elongation | 24% in 2" |
| Total Diffusible Hydrogen | 5.2 ml/100g |
| Shielding Gas | 75% Ar / 25% CO₂ |
| Current Type | DCEN |
| Wire Diameter | 1/16" |
The recommended shielding gas is 75% Argon and 25% CO₂.
Typical tensile strength is 86,100 psi (594 MPa) and yield strength is 68,800 psi (474 MPa).
DCEN (direct current electrode negative) polarity is specified.